


Before01
Company overview
- Handwritten energy logs
- No per-machine data
- No basis for targets
DIGITALIZE
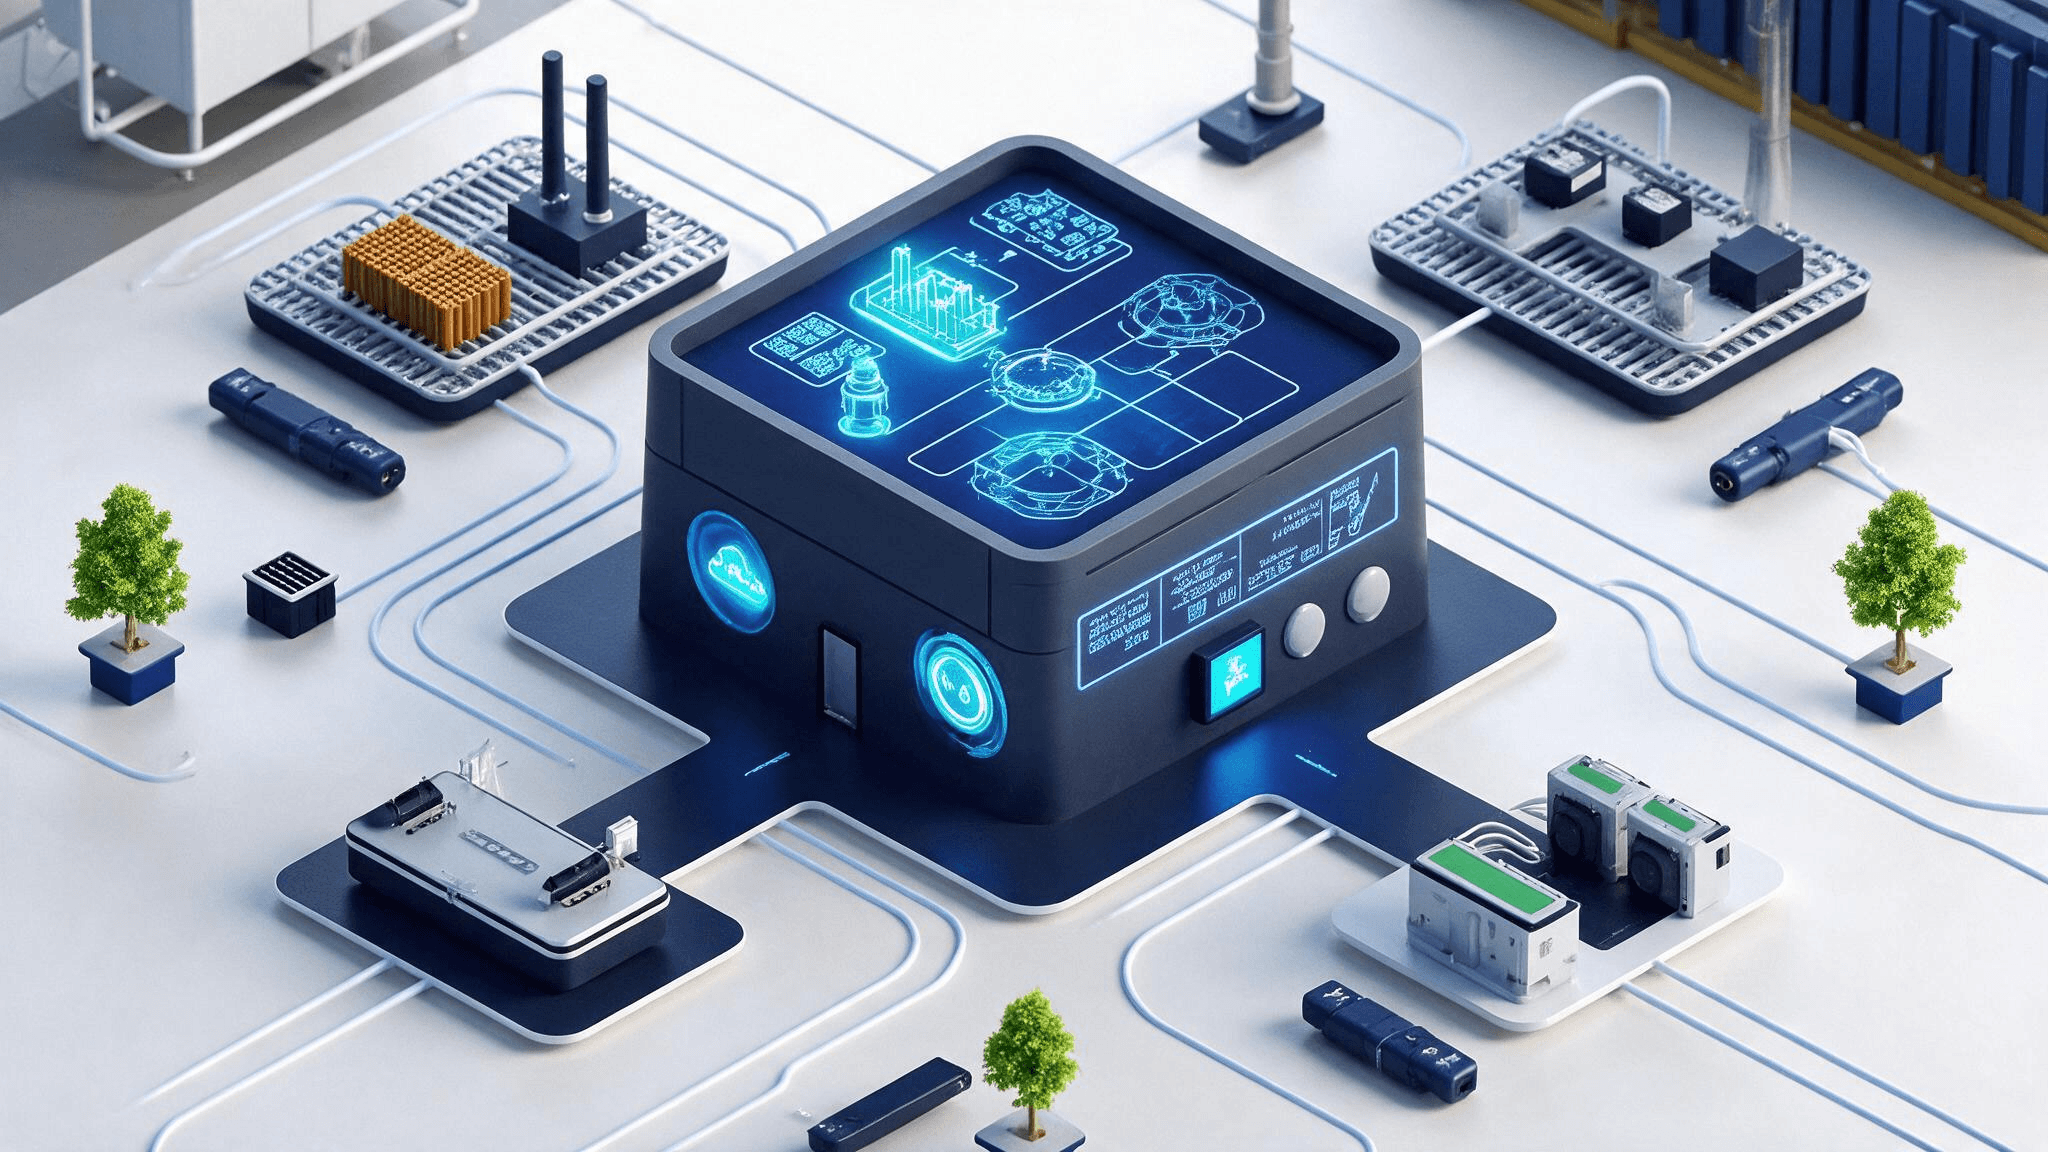
An FEMS solution that transforms energy efficiency on the factory floor
PROCESS
From site assessment through IoT infrastructure and commissioning, the energy management system is built up stage by stage.
EFFECT
Energy costs and carbon emissions come down together, while productivity and equipment operation improve.
Lower energy costs
Real-time monitoring reveals consumption patterns so wasted electricity can be identified · Replacing and upgrading low-efficiency equipment cuts operating costs
Higher output and quality
Linking energy and process data secures consistent quality and reduces the defect rate · Removing bottlenecks raises equipment utilization and available output per production unit
Getting ahead of global environmental regulation
Accurate carbon accounting meets global supply-chain requirements and environmental regulation · Builds credibility and export competitiveness under regimes such as RE100 and CBAM
Optimized equipment operation
Detecting anomalies in consumption patterns enables equipment failures to be predicted and pre-empted · Digitalizes the plant's complex energy flows and applies automatic control logic
CASE STUDY
What FEMS solved at a real site, and what changed afterwards.
Customer industry
Flexible and printed circuit board manufacturing
Before01
After02
Outcomes
An FEMS that turns energy data into savings